Engineering & Application Overview
CNC Hydraulic Press Brakes
A press brake forms sheet or plate by driving a punch into a matched die under controlled force and backgauge position.
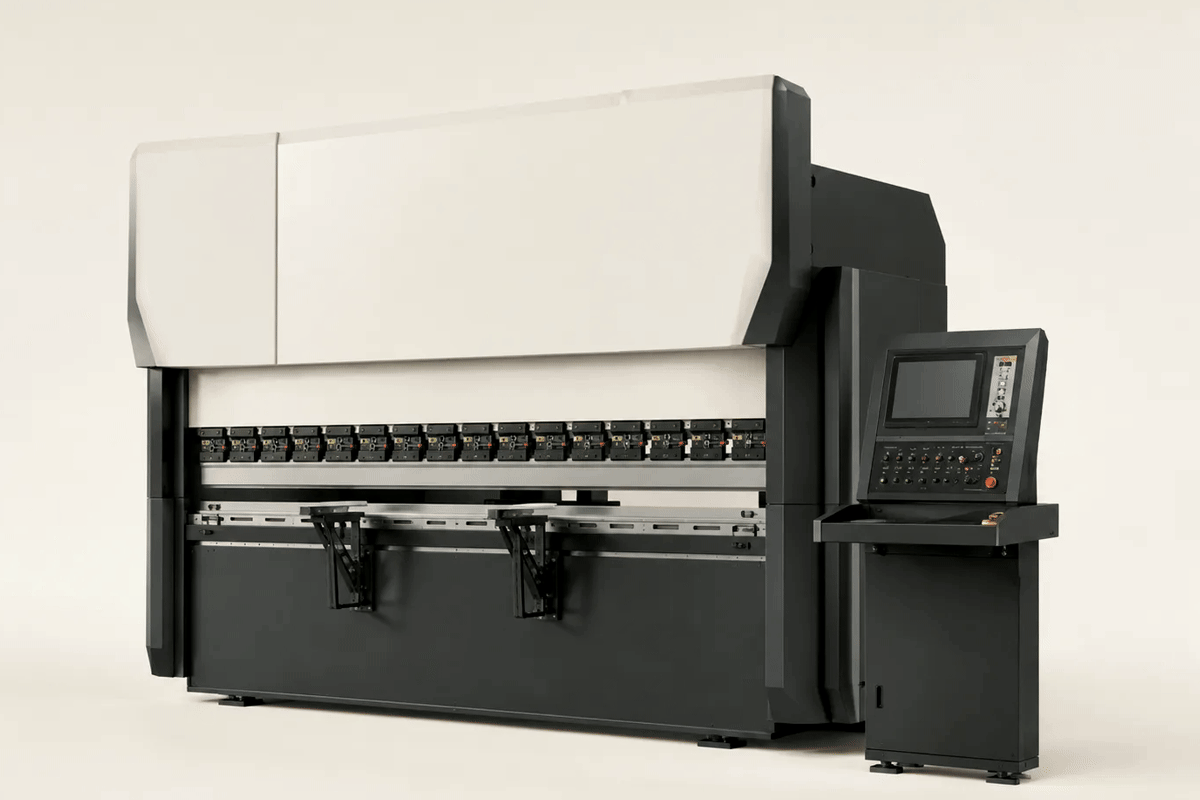
IX-PB-160/3200 is an IXORTA press brake. A press brake forms sheet or plate by driving a punch into a matched die under controlled force and backgauge position. Its principal catalogue values are Press force: 160 ton; Bending length: 3200 mm.
Start with the IXORTA CNC product range, then use this model page to assess fit, operating needs and the information required for a quotation.
IXORTA manufactures specialized industrial configurations engineered in Konya, Türkiye for duty performance, high reliability, and turnkey automation. Explore specific machine types below:
CNC Hydraulic Press Brakes
CNC Hydraulic Press Brakes
CNC Hydraulic Press Brakes
CNC Hydraulic Press Brakes
CNC Hydraulic Press Brakes
CNC Hydraulic Press Brakes
The values below come from the supplied 2026 IXORTA catalogue.
The values below come from the supplied 2026 IXORTA catalogue. Use them to build an initial shortlist, then confirm the exact configuration, options and acceptance criteria in the model-specific quotation.
| Press force | 160 ton |
|---|---|
| Bending length | 3200 mm |
| Stroke | 200 mm |
| Motor power | 15 kW |
Before ordering: confirm the duty, usable capacity, overall dimensions, utilities, safety package, controls, attachments and documentation for the destination market. Download the division catalogue.
IX-PB-160/3200 is the first configuration in a 2-model range; buyers should compare it with the larger listed alternativ...
IX-PB-160/3200 is the first configuration in a 2-model range; buyers should compare it with the larger listed alternatives when production or work-envelope needs may grow.
Shortlist this model when the planned duty is close to its listed values. If the application regularly approaches a limit, compare the adjacent models below and ask IXORTA to check working margin, cycle expectations and future capacity.
The operator selects rated tooling, programs bend sequence and backgauge positions, verifies material and safe clearance...
The operator selects rated tooling, programs bend sequence and backgauge positions, verifies material and safe clearances, then performs a controlled first-piece bend before production.
The safe sequence depends on the supplied guards, controls, utilities and attachments. Operators should follow the delivered manual, training and site risk assessment. For process examples and planning articles, continue to the IXORTA CNC industry guides.
Review frame alignment, ram guidance, hydraulic or drive system, backgauge repeatability, tooling interfaces, guarding a...
Review frame alignment, ram guidance, hydraulic or drive system, backgauge repeatability, tooling interfaces, guarding and safety devices, then verify bends across the useful length.
A useful factory-acceptance record identifies the agreed configuration, principal components, inspection points, test material or load, observed results, open actions, documentation set, packing method and release approval. See IXORTA CNC project scopes for the wider delivery context.
A catalogue capacity alone is not enough.
A catalogue capacity alone is not enough. IXORTA should receive the normal and peak operating range, site conditions, utilities, operator experience, destination and delivery constraints before recommending a configuration. Review the division buyer FAQs before sending the enquiry.
Use the project enquiry form to identify any required training, commissioning or operator documentation.
Use the project enquiry form to identify any required training, commissioning or operator documentation.
Intervals depend on operating hours, duty, dust, heat, water quality and the surrounding environment.
Intervals depend on operating hours, duty, dust, heat, water quality and the surrounding environment. The delivered manual and component schedules control the final service plan. Send spare-parts and service questions through the IXORTA contact page.
Confirm workpiece material and size, output target, electrical supply, ambient factory temperature, controller preferenc...
Confirm workpiece material and size, output target, electrical supply, ambient factory temperature, controller preference, tooling, extraction or coolant duties, operator skills, destination port and inland delivery route.
For a useful export quotation, include the destination port, inland route, unloading equipment, site access, local standards, document language, commissioning responsibility and critical spare-parts expectation. Browse regional project examples.
Send the intended application, capacity, destination and site conditions. The request is routed to the IXORTA team with this division and model already identified.
Direct engineering answers on durability, climate adaptation, maintenance, and factory delivery from IXORTA in Konya, Türkiye.
A press brake forms sheet or plate by driving a punch into a matched die under controlled force and backgauge position. Typical applications include sheet-metal bending, enclosures, fabricated frames, production forming.
The operator selects rated tooling, programs bend sequence and backgauge positions, verifies material and safe clearances, then performs a controlled first-piece bend before production.
Press force is 160 ton; Bending length is 3200 mm; Stroke is 200 mm; Motor power is 15 kW. These are catalogue-listed reference values and must be confirmed in the final quotation.
Send the application, required capacity, materials or operating conditions, utilities, destination country and port, site constraints, preferred options, project timing and installation expectations.
The agreed configuration, safety equipment, dimensions, utilities, documentation, factory acceptance scope, packing, spare-parts list, installation responsibilities and destination requirements should be recorded before release.
Yes. The machine features an IP54 sealed electrical cabinet with an integrated thermostatic heat exchanger/chiller, high-grade Schneider/Omron electronics, and automatic centralized lubrication to ensure precision machining even in demanding 24/7 operating environments.
IXORTA CNC equipment utilizes genuine international components, including Fanuc, Siemens, or Syntec controllers, high-inertia digital servo motors, and precision THK / PMI linear roller guideways with C3-grade preloaded ballscrews.
Prior to container loading, each machine undergoes Renishaw laser interferometer positioning verification, ballbar circularity testing, spindle dynamic balance calibration, and a continuous 72-hour dry-run machining cycle.
Yes. Factory-trained service engineers assist with machine positioning, foundation anchoring, geometric alignment, and G-code / CAD/CAM operator training on-site or via dedicated remote video commissioning.
All machines include an initial tooling and wear-parts kit (protective windows, nozzles, seals). Critical mechanical and electronic spares are stocked in Konya and dispatched worldwide with online remote telemetry diagnostics available 24/7.
Use the enquiry form above, email the technical brief or continue by WhatsApp.